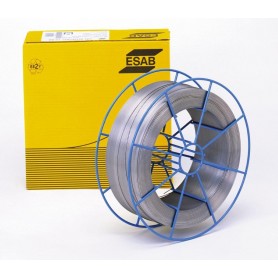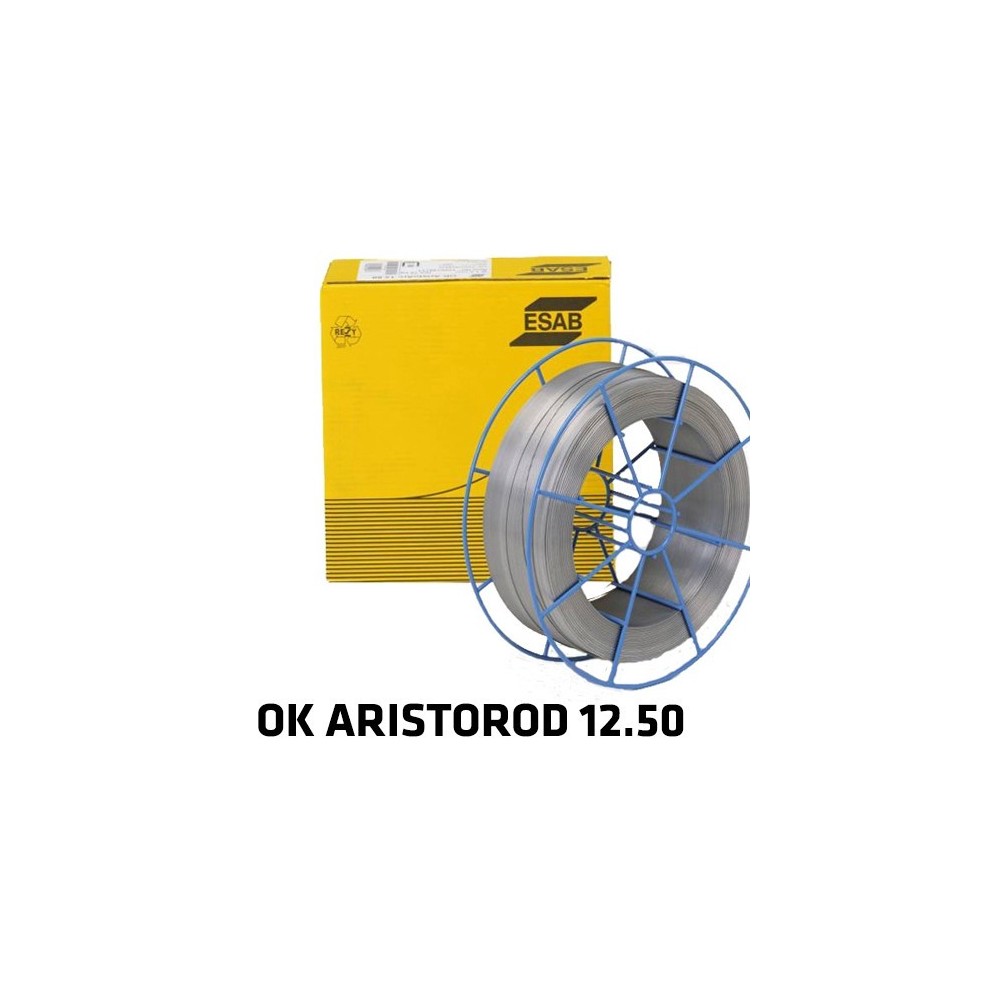
ESAB OK ARISTOROD 12.63 DIAM. 1.0 SG3 MIG MAG WIRE FOR NON-COPPERED CARBON STEELS 18 KG SPOOL
OK AristoRodª 12.63 is a non-copper coated, low alloy Mn-Si wire, G4Si1/ER70S-6, for MAG welding of non-alloy steels such as those for general construction, automotive components, tanks and shipbuilding.
Compared to OK AristoRod 12.50, it has slightly higher manganese and silicon contents and, therefore, a higher tensile strength and a lower sensitivity to impurities present on the surfaces of the pieces to be welded.
OK AristoRodª 12.63 is a non-copper coated, low alloy Mn-Si wire, G4Si1/ER70S-6, for MAG welding of non-alloy steels such as those for general construction, automotive components, tanks and shipbuilding.
Compared to OK AristoRod 12.50, it has slightly higher manganese and silicon contents and, therefore, a higher tensile strength and a lower sensitivity to impurities present on the surfaces of the pieces to be welded.
 Security policy
(edit with the Customer Reassurance module)
 Delivery policy
(edit with the Customer Reassurance module)
 Return policy
(edit with the Customer Reassurance module)
OK AristoRod 12.63 is also produced with a unique technology (ASC - Advanced Surface Characteristics) that allows it to be classified in terms of performance and efficiency at the highest levels especially in mechanized and/or robotic MAG welding. Main characteristics also include excellent properties at the ignition of the arc, the flow in the sheath and a very stable arc even at high currents. Minimal spatter, low smoke emissions and resistance to corrosion equal to that obtained with copper-plated MAG wires.
| Classifications | EN ISO 14341-A : G 42 3 C1 4Si1 EN ISO 14341-A : G 46 5 M21 4Si1 EN ISO 14341-B : G 55A 5 M21 S6 EN ISO 14341-A : G 4Si1 SFA/AWS A5.18 : ER70S-6 CSA W48 : BG 49A 3 C1 S6 EN ISO 14341-B : G S6 |
| Approvals | ABS : 3YSA (C1) ABS : 3YSA (M21) BV : SA3YM (C1 & M21) CE : EN 13479 CWB : BG 49A 3 C1 S6 DB : 42.039.30 DNV-GL : III YMS (C1) DNV-GL : III YMS (M21) LR : 3YS H15 (C1) LR : 3YS H15 (M21) NAKS/HAKC : 1.0 - 1.2MM VdTÜV : 10051 |
| Alloy type | Carbon-manganese steel (Mn/Si-alloyed) |
| Typical tensile properties | |||
|---|---|---|---|
| State | Yield strength | Tensile strength | Stretching |
| EN 80Ar/20CO2 (M21) | |||
| As welded | 490 MPa | 590 MPa | 29% |
| De-stressed 15 hour(s) 650 °C |
385 MPa | 520 MPa | |
| EN CO2 (C1) | |||
| As welded | 460 MPa | 570 MPa | 28% |
| AWS CO2 (C1) | |||
| As welded | 450 MPa | 550 MPa | 30% |
| Charpy V-notch test properties | ||
|---|---|---|
| State | Test temperature | Tenacity value |
| EN 80Ar/20CO2 (M21) | ||
| As welded | -30 °C | 100 J |
| De-stressed 15 hour(s) 650 °C |
-20 °C | 90 J |
| As welded | -50 °C | 80 J |
| As welded | -40 °C | 90 J |
| As welded | 20 °C | 130 J |
| As welded | -20 °C | 120 J |
| De-stressed 15 hour(s) 650 °C |
20 °C | 120 J |
| EN CO2 (C1) | ||
| As welded | 20 °C | 110 J |
| As welded | -30 °C | 75 J |
| AWS CO2 (C1) | ||
| As welded | -30 °C | 100 J |
| typical deposit analysis | |||||
|---|---|---|---|---|---|
| C | Mn | Yes | S | P | Who |
| CO2 (C1) | |||||
| 0.09 | 1.08 | 0.70 | 0.013 | 0.013 | 0.05 |
| Ar/20CO2 (M21) | |||||
| 0.10 | 1.28 | 0.80 | 0.013 | 0.013 | 0.05 |
| Typical Wire Composition % | ||
|---|---|---|
| C | Mn | Yes |
| 0.074 | 1.68 | 0.95 |
| Deposit data | ||||
|---|---|---|---|---|
| Diameter | Amp | Volt | Wire drag speed | Deposit rate |
| 0.8mm | 60-185 A | 18-24V | 3.2-10.0 m/min | 0.8-2.5 kg/h |
| 0.9mm | 70-250 A | 18-26 V | 3.0-12.0 m/min | 0.8-3.3 kg/h |
| 1.0mm | 80-300 A | 18-32V | 2.7-15.0 m/min | 1.0-5.5 kg/h |
| 1.2 mm | 120-380 A | 18-35 V | 2.3-15.0 m/min | 1.2-8.0 kg/h |
| 1.4mm | 150-420 A | 22-36 V | 2.3-12.0 m/min | 1.6-8.7 kg/h |
| 1.6mm | 225-550 A | 28-38 V | 2.3-12.0 m/min | 2.1-11.4 kg/h |